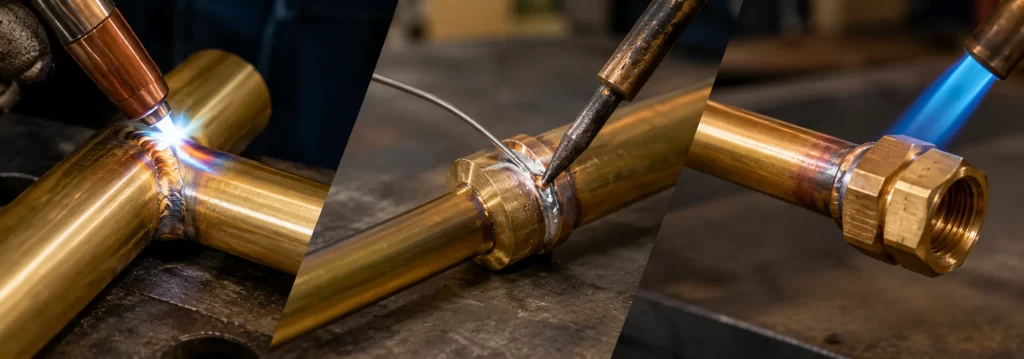
Yes, brass can be joined by heat, but true fusion welding is the hardest way to do it. This guide from Anand Brass Components explains why zinc makes brass tricky, and how to choose between soldering, silver brazing, TIG/MIG brazing and mechanical joints.
⚡ Quick Answer
Can brass be welded?
Yes, but brass is usually brazed or soldered rather than fusion-welded. Zinc boils at about 907 °C, which is at or below brass’s melting range (about 900–940 °C). Melting brass therefore vaporizes zinc, causing porous welds and toxic zinc-oxide fumes. The practical choices are soft soldering (below 450 °C) for low-strength and plumbing joints, silver brazing (about 600–800 °C) for strong, leak-tight joints and brass-to-steel, and TIG or MIG brazing with silicon bronze filler (ERCuSi-A) for heavier repairs. Fusion welding is possible on low-zinc red brass with care. Always use flux, fume extraction and respiratory protection.
“Can I weld brass?” is one of the most common questions we get from fabricators, maintenance teams and hobbyists. The short answer surprises many people: you can, but in most situations you shouldn’t, because there are easier and stronger ways to join brass that don’t fight its chemistry.
At Anand Brass Components we manufacture brass fittings, valves, inserts and electrical parts. Many of them are later soldered, brazed or assembled by our customers. This guide explains what works, what doesn’t, and why, so you choose the right joining method and the right brass grade from the start.
🎯 Key takeaways
- Zinc is the problem. It boils near brass’s melting point, causing porosity and toxic fumes.
- Brazing is usually the best answer. It’s strong, leak-tight and doesn’t melt the brass.
- Soldering suits plumbing, electrical and decorative joints that don’t carry high loads.
- Silicon bronze (ERCuSi-A) is the go-to filler for TIG and MIG brazing brass.
- Leaded free-cutting brass brazes and welds poorly. Choose a low-lead grade if joints are planned.
- Zinc fumes cause metal fume fever. Ventilation and a respirator are essential.
Why brass is hard to weld: the zinc problem
Brass is copper alloyed with zinc, typically 5–45% zinc. The two metals behave very differently when heated:
| Item | Temperature |
|---|---|
| Zinc melts | ~420 °C |
| Soft soldering range | below ~450 °C |
| Silver brazing alloys flow | ~600–800 °C (alloy-dependent) |
| Brass melts (range) | ~900–940 °C (C36000 ≈ 888–899 °C) |
| Zinc boils | ~907 °C |
| Copper melts | 1,085 °C |
Because zinc boils at about the temperature where brass melts, any process that melts the base metal drives zinc out as vapor. That causes three problems:
- Porosity. Zinc vapor bubbles get trapped in the weld, making it weak and leaky.
- Changed chemistry. Losing zinc changes the alloy at the joint, affecting color, strength and corrosion resistance.
- Fumes. Zinc vapor oxidizes instantly into dense white zinc-oxide fume, which causes metal fume fever if inhaled.
Brazing and soldering avoid all three because they don’t melt the brass. Only the filler melts and flows into the joint by capillary action. To understand brass composition in more depth, see What Is Brass? 20 Common Questions Answered.
Brass joining methods compared
| Method | Melts brass? | Typical temperature | Joint strength | Best for |
|---|---|---|---|---|
| Soft soldering | No | < 450 °C | Low–moderate | Plumbing, electrical, decorative, sealing |
| Silver brazing | No | ~600–800 °C | High | Pressure joints, HVAC, brass-to-steel, precision assemblies |
| Brass (bronze) brazing with RBCuZn rod | No (close to the limit) | ~870–900 °C | High | Repair of fittings and castings, heavier sections |
| TIG/MIG brazing (silicon bronze) | Minimal | Filler ~1,000 °C, low heat input | High | Repairs, thicker parts, joining to steel |
| Fusion welding (TIG/oxy-fuel) | Yes | Above melting range | Variable (porosity risk) | Low-zinc red brass, specialist repairs |
| Mechanical (threads, press-fit, crimp) | No heat | — | High (by design) | Most fittings, inserts, terminals |
Soldering brass
Soft soldering joins brass with a low-melting filler, typically tin-based, below about 450 °C. Brass solders well because it wets easily once clean.
What solder to use on brass
- Plumbing and drinking water: use lead-free solder, such as tin-copper or tin-silver-copper alloys, with a compatible flux. In the US, solder and flux used on potable-water systems must contain no more than 0.2% lead.
- Electrical and electronics: use lead-free tin-silver-copper (SAC) solder with a rosin or no-clean flux.
- Decorative and model work: tin-based solder with an active flux. Clean off flux residue afterwards to prevent corrosion.
Tips for good solder joints
- Clean both surfaces to bright metal with fine abrasive or a wire brush. Oxide stops the solder wetting.
- Apply flux immediately after cleaning.
- Heat the brass, not the solder. Touch the solder to the hot joint and let capillary action pull it in.
- Don’t overheat. Burnt flux stops flow.
- Wash off flux residue, especially acid fluxes.
Brass conducts heat well, so large fittings soak up heat. Use a torch or iron with enough power, and preheat bigger parts rather than holding a small iron on them for minutes.
Brazing brass: the strongest practical joint
Brazing uses a filler that melts above 450 °C but below the base metal’s melting point. For brass there are two main families.
Silver brazing (BAg alloys)
Silver-bearing brazing alloys flow at roughly 600–800 °C, well below the melting range of brass. That makes them ideal: the brass stays solid, zinc doesn’t boil off, and joints are strong, ductile and leak-tight. Silver brazing is the standard for brass-to-copper and brass-to-steel joints in HVAC, refrigeration, instrumentation and precision assemblies. Use a fluoride-based flux suited to the alloy.
Brass or “bronze” brazing (RBCuZn alloys)
Copper-zinc brazing rods such as RBCuZn-A flow at about 870–900 °C. They’re cheaper than silver alloys and common for repairing brass fittings and castings. The working window is narrow, because you’re close to the melting point of the brass itself. Use a slightly oxidizing oxy-fuel flame and good flux, and work quickly to limit zinc fuming.
Copper-phosphorus brazing alloys (BCuP) are popular for copper-to-copper joints without flux. On brass they need a flux, and they should not be used on steel or other ferrous metals, where they form brittle phosphides.
Planning to braze or solder your brass parts?
Tell us your joining process. Anand Brass Components will recommend a brass grade that brazes cleanly and machine the parts to your drawing.
TIG and MIG brazing brass with silicon bronze
TIG or MIG brazing uses an arc instead of a gas torch, with a silicon bronze filler (AWS ERCuSi-A). The filler melts at a lower temperature than steel filler wires and bonds to the base metal mainly by wetting rather than full fusion, so heat input stays low. Its deposit doesn’t depend on zinc, so zinc lost from the base metal doesn’t spoil the joint chemistry.
- TIG: DC electrode-negative with 100% argon shielding is the usual setup. Keep heat input low, travel quickly, and keep gas coverage over the hot zone.
- MIG brazing: ERCuSi-A wire is suited to thinner brass and to joining brass to steel or galvanized steel.
- Strength: brazed joints are strong but generally not as strong as full fusion welds in steel. Don’t use them where structural code welds are required.
Silicon bronze also gives a close color match on many brasses, which helps for decorative repairs. For more on how bronze and brass differ, see Brass vs Bronze.
Fusion welding brass: when it’s possible
True fusion welding, where the base metal melts, is possible but difficult. It’s most practical on low-zinc brasses such as red brass (about 15% zinc). High-zinc yellow brasses (30–40% zinc) are generally better brazed than welded.
If you must fusion-weld brass:
- Use TIG with argon shielding and a silicon bronze (ERCuSi-A) filler, which tolerates zinc loss. ERCu filler can give a closer color match on red brass.
- With oxy-acetylene, a slightly oxidizing flame forms a zinc-oxide skin that reduces zinc boil-off.
- Keep heat input low and travel fast to limit the molten zone.
- Expect some porosity, and test pressure-bearing parts.
- Use local fume extraction and a respirator rated for metal fume.
How the brass grade affects joining
The grade you buy has a big effect on how well it brazes or welds. This is where buyers can avoid problems before parts are made:
| Grade | Soldering | Brazing | Fusion welding | Notes |
|---|---|---|---|---|
| C36000 / CW614N free-cutting (≈3% lead) | Good | Fair–poor | Not recommended | Lead can cause hot cracking and poor wetting at brazing temperatures |
| CW617N forging brass (≈2% lead) | Good | Fair | Not recommended | Common for valve bodies that are soldered or brazed |
| C26000 cartridge brass (70/30, low lead) | Excellent | Good | Fair | Good choice for brazed assemblies |
| C23000 red brass (85/15) | Excellent | Excellent | Good (best among brasses) | Low zinc means less fuming |
| C69300 lead-free silicon brass | Good | Good | Fair | Popular for potable-water parts |
| CW602N DZR brass | Good | Fair | Not recommended | Check that brazing heat doesn’t reduce DZR performance |
General guidance; joinability also depends on section size, joint design and process. Confirm with trials for critical joints.
For help choosing grades, see Brass Alloy Grades Explained, Brass Alloy for CNC Machining and Lead-Free Brass Components.
Joining brass to steel, copper and stainless steel
- Brass to copper: soft solder for plumbing, silver braze for pressure and HVAC joints. Both metals braze easily.
- Brass to mild steel: silver brazing is the most reliable method. TIG or MIG brazing with silicon bronze also works well. Don’t use phosphorus-copper alloys on steel.
- Brass to stainless steel: silver brazing with a flux formulated for stainless steel. Stainless steel’s oxide layer needs an aggressive flux.
- Brass to aluminium: difficult. Use mechanical joints or specialist processes instead.
Step-by-step: how to silver braze brass
Design a lap or socket joint
Brazing relies on capillary action. Aim for a clearance of roughly 0.05–0.15 mm and an overlap of about three times the thinner wall.
Clean the surfaces
Degrease, then abrade to bright metal. Braze soon after cleaning, before oxide forms.
Apply flux
Coat both joint surfaces with a flux suited to the brazing alloy. Flux prevents oxidation and helps the filler flow.
Fit and support
Assemble the joint and fixture it so it can’t move while the filler solidifies.
Heat evenly
Heat the whole joint area with a broad torch flame, concentrating on the heavier part. The flux turning clear and liquid shows you’re near brazing temperature.
Feed the filler
Touch the brazing rod to the joint, not the flame. It should flow into the gap. Stop once a small fillet forms all round.
Cool and clean
Let the joint cool naturally, then remove flux residue with hot water and a brush. Fluoride fluxes are corrosive if left on.
Inspect and test
Check for a continuous fillet, and pressure-test fluid-carrying joints.
Filler metals and fluxes for brass
| Filler (AWS / type) | Process | Approx. working range | Use on brass |
|---|---|---|---|
| Lead-free tin-copper / tin-silver-copper solder | Soft soldering | ~220–300 °C | Plumbing, electrical, decorative |
| Silver brazing alloys (BAg series) | Torch / induction brazing | ~600–800 °C | Strong pressure joints; brass to copper, steel, stainless |
| Copper-zinc rod (RBCuZn-A) | Oxy-fuel brazing | ~870–900 °C | Repairing brass fittings and castings |
| Silicon bronze (ERCuSi-A) | TIG / MIG brazing or welding | Arc; low heat input | Repairs, thicker sections, brass to steel |
| Copper (ERCu) | TIG welding | Arc | Color match on red brass |
| Copper-phosphorus (BCuP) | Torch brazing | ~700–850 °C | Brass to copper only, with flux. Never on steel |
Ranges are approximate. Follow the filler manufacturer’s data sheet for exact solidus, liquidus and recommended brazing temperature.
Choosing a flux
- Soldering: water-soluble or rosin fluxes for electrical work, and potable-water-approved fluxes for plumbing. Remove residues after soldering.
- Silver brazing: fluoride-based paste fluxes, with “black” high-temperature fluxes for longer heating cycles or larger parts.
- Copper-zinc brazing: borax-based fluxes, often supplied as flux-coated rods.
- TIG/MIG: no flux. Argon shielding gas protects the joint.
Troubleshooting brass joints
| Problem | Likely cause | Fix |
|---|---|---|
| Porous or bubbly joint | Brass overheated; zinc boiling | Lower heat, switch to silver brazing or TIG brazing |
| Filler balls up and won’t flow | Dirty surface or exhausted flux | Re-clean to bright metal, apply fresh flux |
| Cracks near the joint | High-lead brass, or stress during cooling | Use low-lead grade, support the joint, cool slowly |
| White powder or smoke | Zinc oxide from overheating | Reduce temperature; improve fume extraction |
| Pink or copper-colored patch | Zinc lost from surface (dezincified by heat) | Lower heat input; shorten heating time |
| Joint leaks under pressure | Gap too large or too small, incomplete penetration | Correct the joint clearance; heat the joint evenly |
| Green or corroded joint later | Flux residue left on part | Wash off flux thoroughly after joining |
| Plating blistered or discolored | Part plated before brazing | Plate after all hot work is complete |
Inspecting and testing brazed brass joints
For production joints, especially in gas, water or pressure service, inspection matters as much as technique:
- Visual check: look for a smooth, continuous fillet all around the joint, with no gaps, pinholes or flux inclusions.
- Pressure or leak testing: air-under-water, pressure-decay or helium leak tests for fluid-carrying parts.
- Sectioning: cut sample joints during process qualification to confirm filler penetration.
- Process control: fixed joint clearances, flux quantity, heating time and temperature give repeatable joints. Induction brazing is common in volume production for this reason.
Anand Brass Components machines brass parts to tight, repeatable tolerances (±0.01 mm), which helps brazing clearances stay consistent from part to part. See our quality & approvals page.
Fume safety: zinc and metal fume fever
Overheated brass gives off zinc-oxide fume, the white smoke you may see at the torch. Breathing it can cause metal fume fever, a flu-like illness with fever, chills, nausea and aching that usually starts a few hours after exposure. Other hazards include lead fume from leaded brasses and cadmium from some older silver brazing alloys.
- Work with local exhaust ventilation that captures fume at the source, or outdoors.
- Wear a respirator rated for metal fume when brazing or welding brass.
- Use cadmium-free brazing alloys.
- Don’t overheat. Keep the brass below its melting range when brazing.
- Follow your local occupational safety rules and the product safety data sheets.
If you develop fever or breathing symptoms after welding or brazing, stop work, get fresh air and seek medical advice.
Best joining method by application
| Application | Usual method | Notes |
|---|---|---|
| Domestic water plumbing | Threaded, compression or lead-free soft solder | Use potable-water-approved solder and flux |
| HVAC & refrigeration | Silver brazing | Pressure- and vibration-resistant joints |
| Gas & LPG fittings | Threaded with approved sealant; brazing where specified | Follow gas codes; never improvise gas joints |
| Electrical terminals & connectors | Crimp, screw clamp or soft solder | Keep heat away from insulation and plating |
| Instrumentation & sensors | Silver brazing or induction brazing | Tight, repeatable joint clearances |
| Marine fittings | Threaded or silicon-bronze TIG brazing | Choose naval or DZR brass grades |
| Musical instruments | Soft solder (and silver solder for some joints) | Specialist repair work |
| Jewellery & décor | Silver solder or soft solder | Small torch, careful flux cleanup |
| Castings repair | RBCuZn brazing or silicon-bronze TIG brazing | Preheat larger castings evenly |
Myths about welding brass
- “Brass can’t be welded.” It can. It just needs the right method, and brazing is usually the better choice.
- “Brazing is weaker than welding, so it’s second-best.” A properly designed brazed lap joint in brass is often stronger than the parent metal next to it.
- “Any solder works on brass.” Drinking-water systems need lead-free solder, and acid fluxes must be cleaned off.
- “The white smoke is harmless steam.” It’s zinc-oxide fume, which can cause metal fume fever.
- “More heat makes a better joint.” Overheating brass boils off zinc and ruins the joint.
Mechanical alternatives: often the best “joint” of all
Most brass components are designed so they never need heat at all. Brass machines into precise, leak-tight threads and accepts knurls, crimps and press fits well:
- Threaded joints: BSP, NPT and metric threads on fittings and hose fittings.
- Compression joints: ferrule-and-nut fittings seal without solder.
- Molded-in inserts: brass inserts for CPVC, UPVC and PPR fittings lock into the plastic during molding.
- Crimp and screw terminals: electrical terminals and connectors.
- Press-fit and riveted assemblies: fast and repeatable for high volumes.
Mechanical joints avoid heat damage, fumes and changes to the alloy, and they can be dismantled for service.
Design tips for buyers of brass parts that will be joined
- Tell your supplier the joining method. It changes the grade we recommend.
- Avoid high-lead grades for brazed joints. Choose low-lead or lead-free brass where joints will be brazed.
- Design the joint clearance into the drawing. Capillary gaps for brazing should be specified, not left to chance.
- Plan the plating sequence. Plate after brazing, because brazing heat damages most platings.
- Consider a mechanical joint first. Threads or compression fittings may remove the need for heat entirely.
Learn how we take drawings to production in How Custom Brass Components Are Manufactured for OEMs.
Brass parts engineered for your assembly process
Anand Brass Components: in-house OES alloy control, CNC machining to ±0.01 mm, ISO 9001 certified, exporting to 30+ countries.
Frequently Asked Questions
Related guides
Written by the Anand Brass Components Technical Team. Anand Brass Components is a brass parts manufacturer and exporter at Plot 4110-4111, H-Road, GIDC Phase-III, Jamnagar, Gujarat 361004, India. Founded in 1991, ISO 9001 certified. Contact: info@anandbrass.com · +91 78743 05684.
Safety disclaimer: Welding, brazing and soldering involve heat, fumes and fire risk. This article is general guidance, not a substitute for training, the filler manufacturer’s instructions, safety data sheets or local regulations. References: Miller Electric, “TIG Brazing With Silicon Bronze”; Welders Supply, “Welding Bronze and Brass: Filler Matching by Alloy Type”; Copper Development Association alloy data; general metallurgical references on zinc volatility.